Cold Room Humidification Systems
Maintaining the right humidity level is essential for preserving product quality in cold rooms and cold storage facilities. Cold Room Humidification helps manage moisture levels in the air, reducing excessive dehydration and supporting suitable storage conditions for products that require controlled temperature and humidity. When combined with appropriate refrigeration, ventilation, and hygiene practices, effective humidity management can help maintain product freshness and reduce moisture loss.
Mist Cooling System India provides misting, cooling, and humidification solutions for various industrial and commercial applications. The right system depends on the type of products stored, room dimensions, operating temperature, required humidity range, and storage duration.
Reliable Cold Room Humidification Systems
Cold Room Humidification Systems are designed to introduce controlled moisture into the air when humidity levels fall below the desired range. These systems may be suitable for selected applications in food storage, vegetable and fruit storage, floriculture, agricultural produce facilities, and other temperature-controlled environments.
Maintaining suitable humidity can help reduce dehydration and weight loss in moisture-sensitive products. However, humidity requirements differ by product, and excessive moisture can lead to condensation, mould growth, or other storage problems. Therefore, humidification equipment should be selected according to product specifications and the operating conditions of the cold room.
Get Quote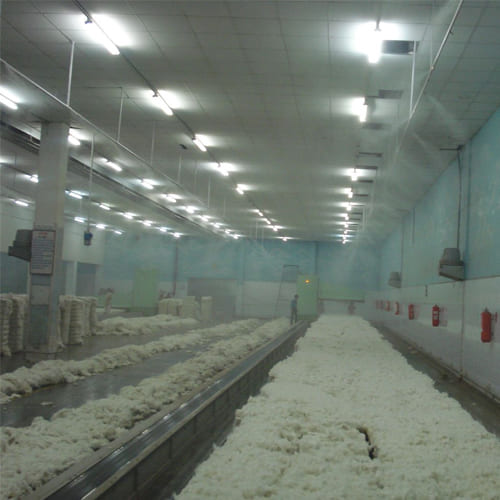
Humidification plant, Misting fan, Sanitization Booth, Sanitization Tunnel
Cold Storage Humidity Control System
A dependable Cold Storage Humidity Control System helps monitor and manage moisture levels alongside temperature regulation. Humidity sensors and suitable control equipment can support more consistent conditions when properly configured. The system should work in coordination with refrigeration and airflow to avoid condensation on walls, ceilings, products, and equipment.
Before choosing a solution, consider storage capacity, temperature settings, airflow patterns, water quality, sensor placement, and cleaning requirements. Regular maintenance and suitable water treatment can help support hygienic operation and consistent performance.
Cold Room Humidification Manufacturers
When searching for Cold Room Humidification Manufacturers, evaluate system suitability, humidity control capabilities, installation requirements, energy and water use, and ongoing maintenance support. An appropriately designed system can help businesses manage storage conditions more effectively.
Cold Room Humidification Suppliers
Mist Cooling System India helps customers explore suitable misting, cooling, and humidification solutions based on their application requirements. Whether you manage a cold room, food storage facility, or agricultural produce warehouse, selecting the right configuration is important for reliable humidity management.
Looking for cold room humidification solutions? Contact Mist Cooling System India to discuss your requirements and identify a suitable approach to cold room and cold storage humidity control.
How humidification plant for textile Works
FAQ's
Humidification is the artificial regulation of humidity in environments. When the atmosphere becomes too dry, moisture is drawn from surrounding materials within the environment such as furniture, paper, textiles, fruit, animals and even people.
Cotton and linen have to be processed at very high levels, around 70-80%RH, because they are very brittle. By humidifying each process, from the combing of the raw material, through carding, twisting, spinning and weaving, the manufacturer can ensure that the product remains flexible and is prevented from breaking.
advantages of using air humidification plant for textile industry: *Reduces production downtime. *Increases productivity and product quality. *Protects against dangerous electrostatic discharge. *Creates a healthy and pleasant working environment for operational staff.
Applications

Indoor Mist Cooling System
In todays modern world uses the same principle of evaporative cooling to reduce temperatures for Patios, Hotels.

Green House Fogging / Propagation Misting System
Professional growers know that it is vital to monitor and control all environmental factors that can affect their crops.

Adiabatic Cooling Kit / Pre-cooling of Air Cooled Condenser
Engineering is a professional discipline that deals with the consec adipis elit sed do eiusmod tempor incididut labore et dolore.

Livestock Cooling Systems
FOR CATTLE / GOAT / PIG FARMS: VAI mist cooling system reduce heat stress thereby providing improved.

Dust Suppression Systems
Fugitive dust (PM10 and subPM10) in the workplace is a major hazard for most industries. Failure to address any of.
Industrial Mist Cooling
In many workplaces, high temperature is the cause of both labor and machinery decline. Additionally, the floating small particles.

Industrial Odor Control System
Many industries have odor control issues. Some of these industries have rules and regulations that must be met to

Fogging System For Humidification in Textile, Spinning & Weaving Mill
Professional growers know that it is vital to monitor and control all environmental factors that can affect their crops.

Moisture System
Properly maintained moisture system levels, will result in improved quality and minimal downtime or rejection.

Fan and Pad Cooling System
We fabricate qualitative range of Fan, Pad Evaporative Cooling System. It is used to cool the air by using the heat present